
Navigation
Cleanroom Engineering for Laboratories
product description
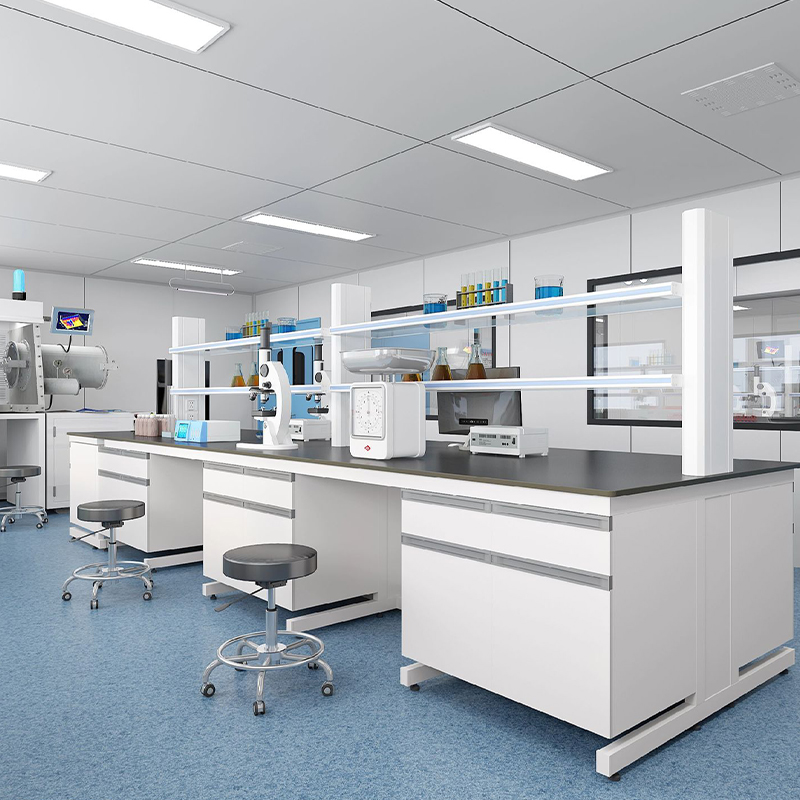
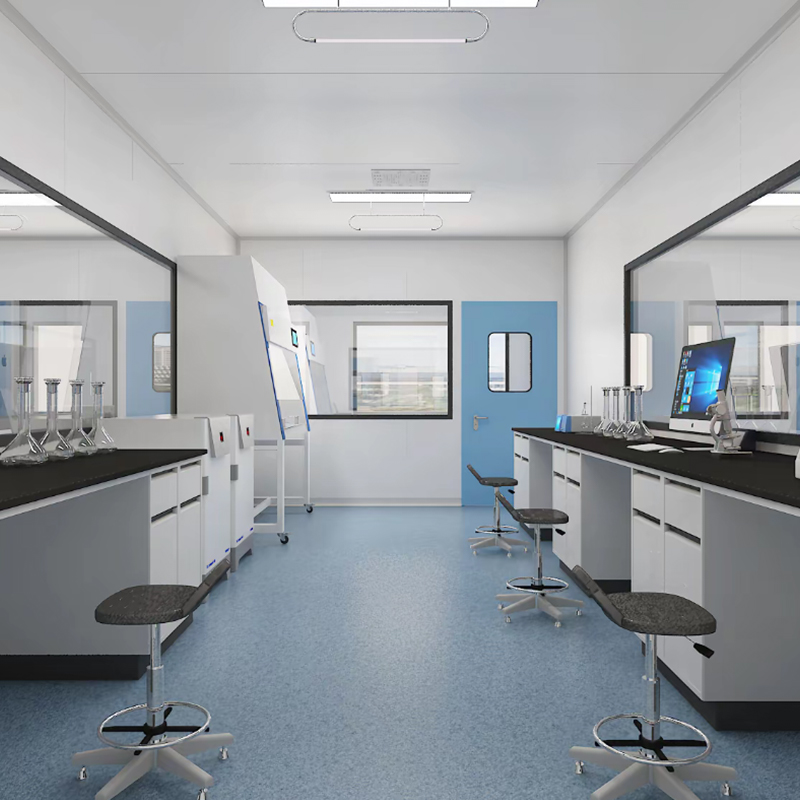
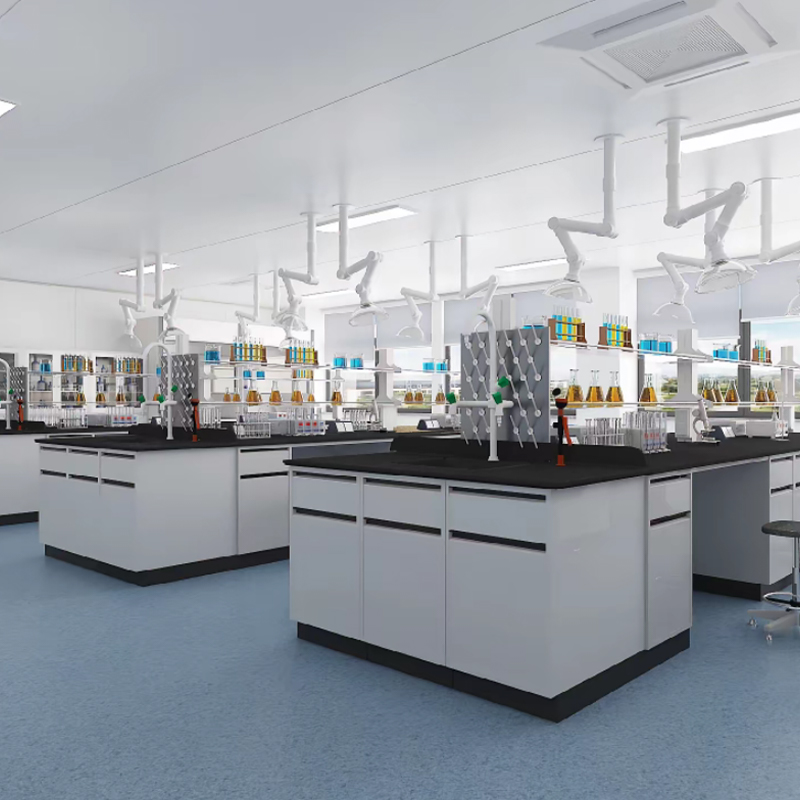
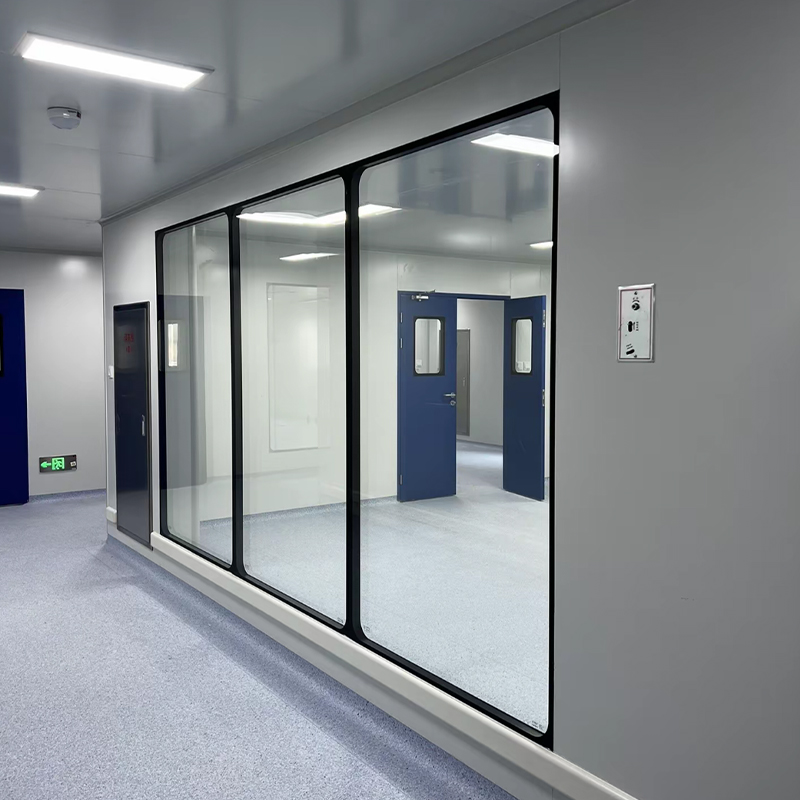
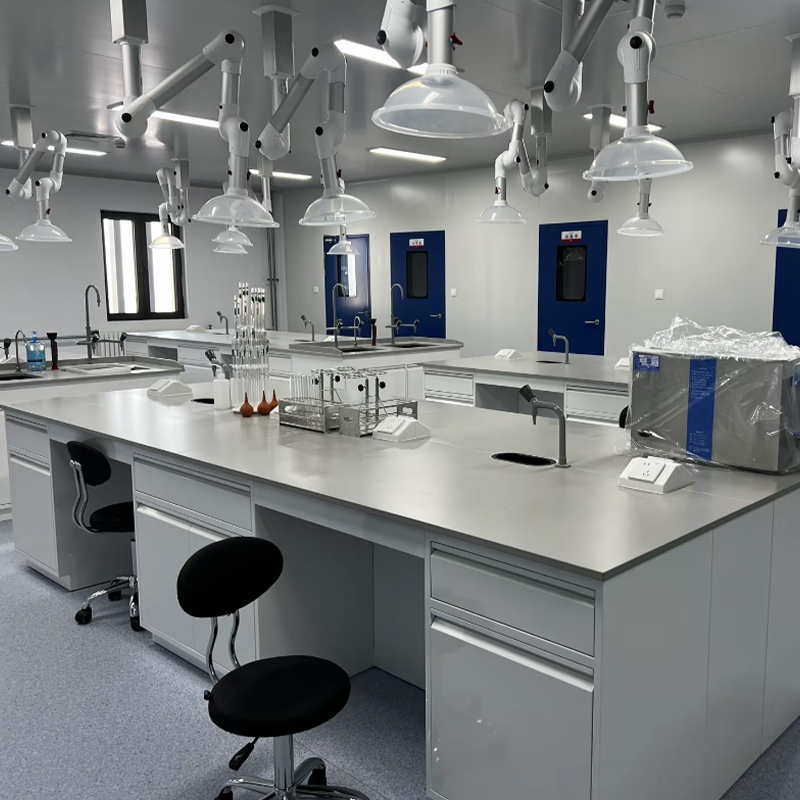
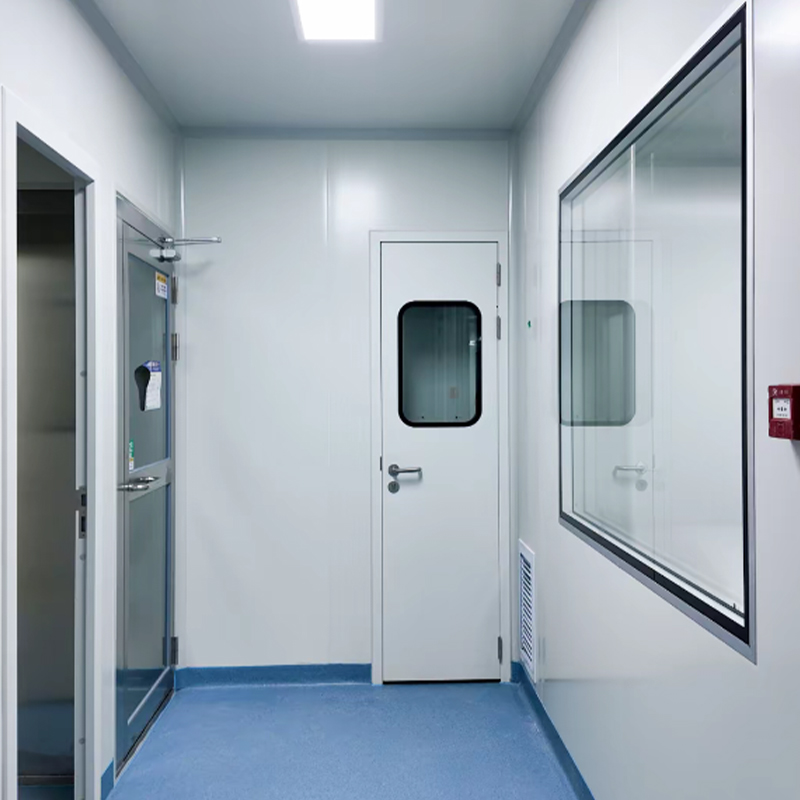
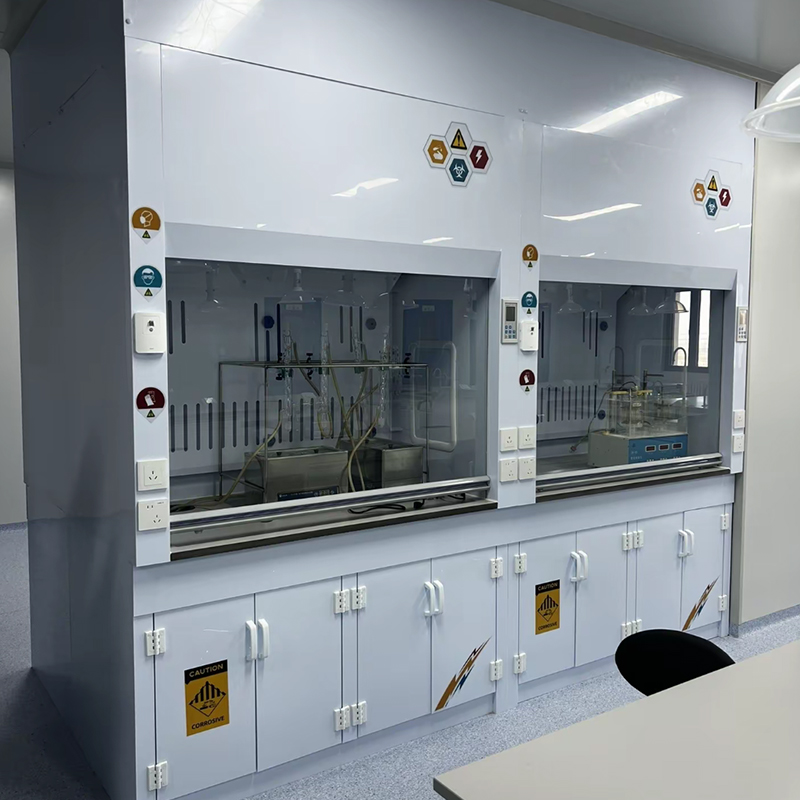
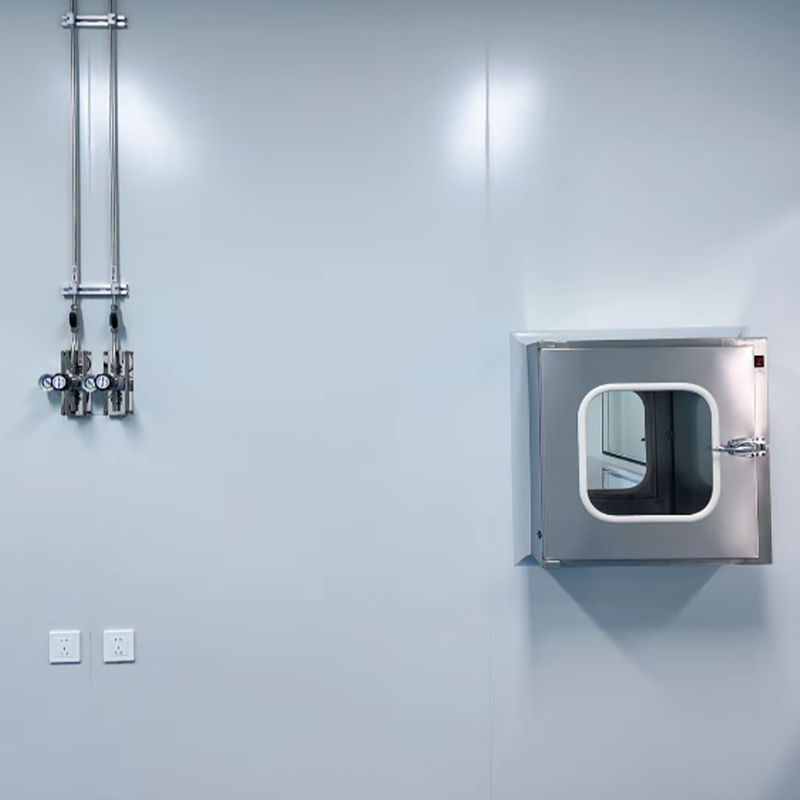
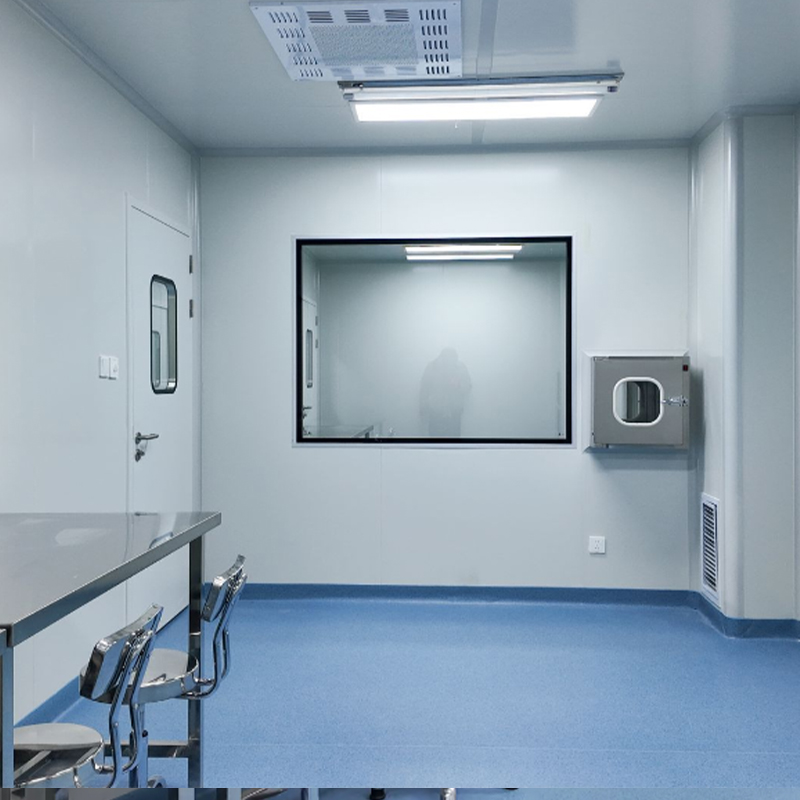
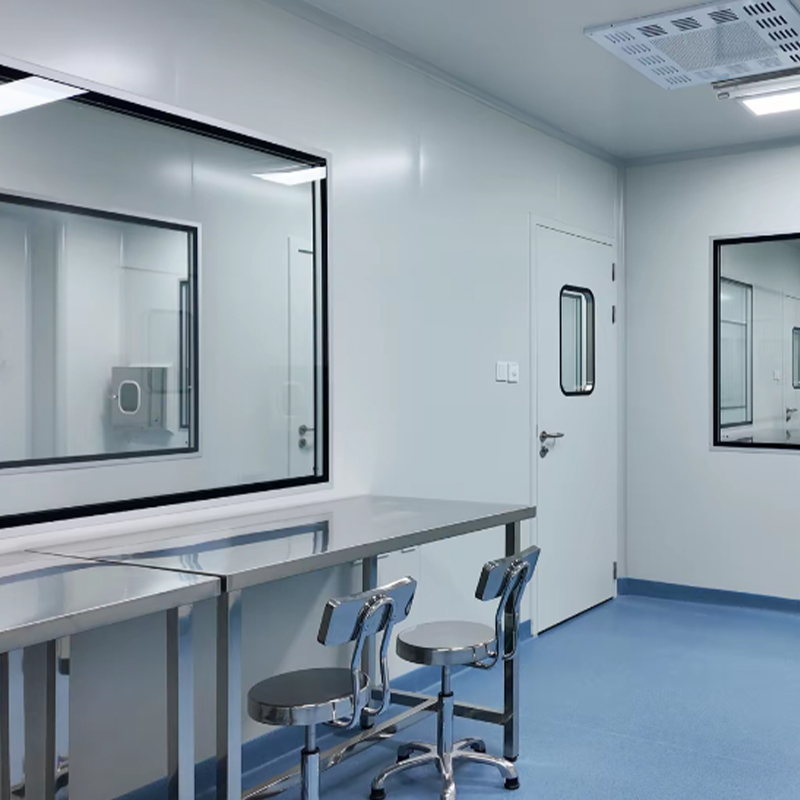
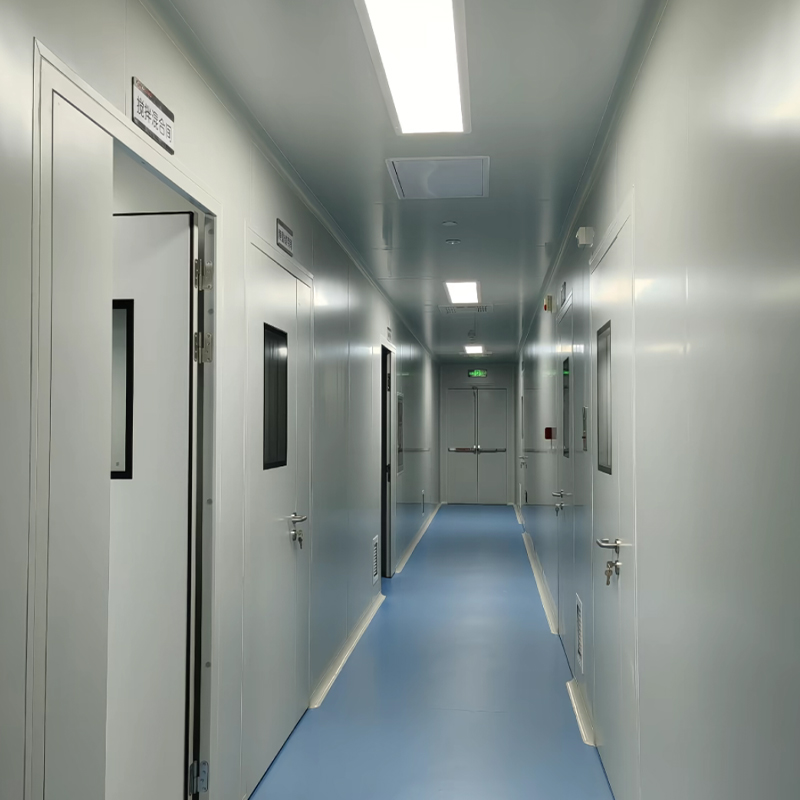
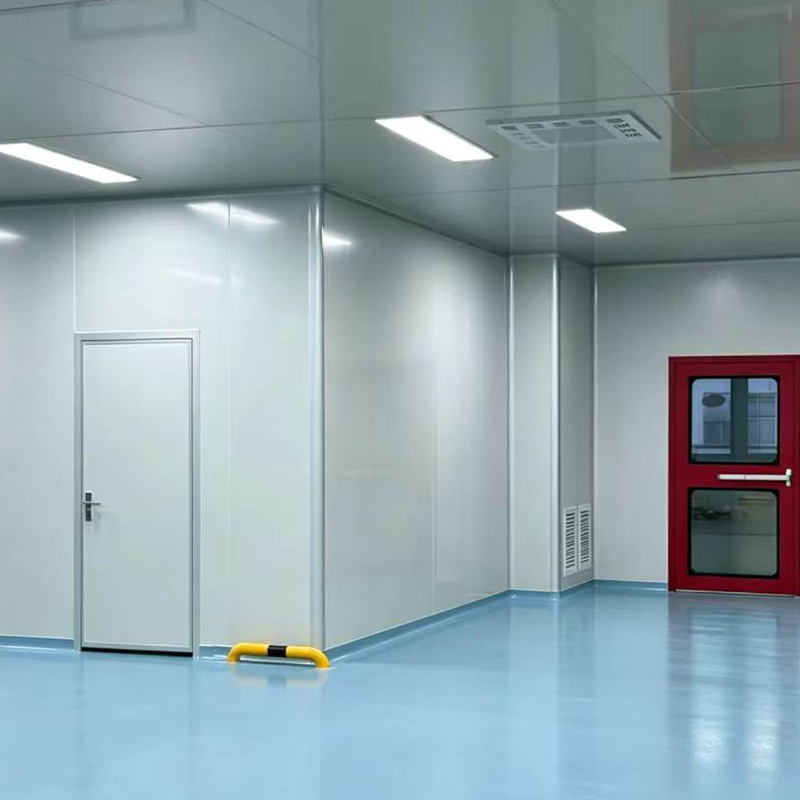
GMP Standard Laboratory Cleanroom – For production scenarios involving vaccines, biologics, in vitro diagnostic reagents, and more, we provide comprehensive cleanroom solutions compliant with China GMP, EU cGMP, and US FDA dual certification standards. This solution integrates production process flows, product cleanliness requirements, and production capacity planning objectives to precisely delineate four-grade clean production zones (A/B/C/D). For critical processes such as sterile filling, lyophilized preparation, and sterile assembly, it implements a cleanroom classification gradient ranging from Class 100 to Class 100,000, fully aligning with the production compliance requirements of diverse medical products. The enclosure system employs modular electrolytic steel plate cleanroom wall panels, complemented by rounded transition edges and seamless epoxy anti-static flooring, ensuring no sanitary dead zones and meeting stringent daily cleaning/disinfection and pressure differential control requirements for production areas. The air purification system features variable frequency drive automation, integrated with four-stage filtration devices (pre-filter, medium-efficiency filter, sub-high-efficiency filter, and high-efficiency filter), achieving a filtration efficiency of 99.99% for 0.3μm particles, while delivering temperature and humidity control accuracy of ±0.5°C and relative humidity control accuracy of ±3%—fully satisfying the high precision demands of biological product production regarding environmental parameters. The accompanying personnel purification system, material purification system, and waste gas/liquid treatment system all incorporate automated interlock designs, eliminating cross-contamination risks at the source. During project delivery, all parameters are traceable and auditable, fully complying with pharmaceutical production regulatory review requirements. This solution empowers medical manufacturing enterprises to achieve efficient, compliant, and stable production capacity, thereby establishing a robust foundational safeguard for the quality and safety of medical products.
FAQ
1. What are your core advantages for medical purification and protection projects?
We integrate independent production, engineering design and overseas service, with mature manufacturing experience in cleanroom and radiation shielding products. We deliver cost-effective, high-standard solutions with stable quality and full compliance for global medical and industrial projects.
2. What customization services can you provide for engineering projects?
We support full-project personalized customization, including door size, shielding thickness, airtight grade, color matching, panel style and installation structure. We can design exclusive solutions according to local construction standards, room layout and customer’s functional requirements.
3. How do you ensure safe overseas transportation?
All export products adopt multi-layer professional packaging with waterproof, shockproof, rust-proof and reinforced wooden box protection. It effectively avoids damage during long-distance sea and air transportation.
4. Can you provide full export customs clearance documents?
Yes. We supply complete export documents including invoices, packing lists, certification files and test reports, assisting clients with smooth customs clearance and project filing.
5. What engineering projects can you undertake?
We undertake full turnkey radiation protection and cleanroom purification projects, covering hospital construction and renovation, laboratory upgrading, pharmaceutical and electronic dust-free workshops, providing one-stop integrated engineering services.
Recommendation
 WhatsApp : +86 17763513578Cleanroom Engineering for Pharmaceutical Plants
Read Article
 WhatsApp : +86 17763513578Cleanroom Engineering for Food Processing Plants
Read Article
 WhatsApp : +86 17763513578Cleanroom Engineering for Laboratories
Read Article
Contact Us
Please give us a message